Temperature Transmitters in Harsh Industrial Environments: A Complete Selection Guide
A faulty temperature transmitter in an offshore platform can shut down production for two straight days and more than $200,000 in lost revenue. The transmitter itself might only cost a few hundred dollars, but the results of being right on the specification are nothing short of catastrophic.
If you’ve ever specified instrumentation for a refinery, or power stations, or steel mills, or oil and gas facilities, you already know this. Likewise, you also noted that specifying a temperature transmitter for really harsh industrial places is certainly not only about the accuracy figure mentioned on the datasheet. It’s about being able to withstand vibration, corrosive media, infernal heat, driving rain, and still send out a good 4–20 mA or HART signal to the control room.
This guide shows in depth how to choose a temperature transmitter that thrives where most electronics do not. You’ll learn when an RTD works better than a thermocouple, how to choose between a head-mount or a field-mount transmitter in your application, what wetted materials are suitable for your reproductive media, and how to integrate the correct signal output to your SCADA or BMS.
What Is a Temperature Transmitter for Harsh Industrial Environments?
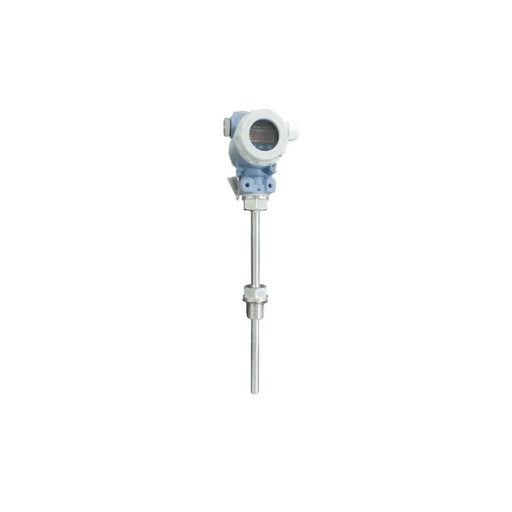
An instrument for harsh industrial climates, temperature transmitter is an instrument that converts a signal of temperature sensor to a robust 4–20 mA or HART output while withstanding extreme vibration, corrosive media, high ambient temperatures, and moisture. In general, such a configuration includes IP67 or IP68 sealing, 316L stainless steel or Hastelloy wetted parts, and ATEX or IECEx hazardous area certification.
What Makes a Temperature Transmitter “Harsh Environment” Rated?
The aluminum of any transmitter does not automatically qualify it as one with a strong enclosure. The wondered temperature transmitter will retain the processed reading throughout its ordeal of being struck by the elements around.
Here are things that it must have to strip any meaning of argument on any kind of measure:
- How well it is sealed. Can a transmitter with an IP65 protection be used in an industrial environment that is flooded, dirty, and has dust particles floating about frequently? Why not maintain the Medium Performance found in all IP67 class members? IP68 can withstand continuous water immersion. When exposed to salt or other harsh chemicals, the NEMA 4 test with either the UV-resistance offered by Epoxy powder coat paint, more polymers on inner and outer parts, and improving gasket design or where due consideration for the NEMA 4X equivalent must be considered.
- Ambient conditions. This is far more important. The electronics inside the transmitter must survive the ambient environment surrounding the transducer, and the temperature inside whatever pipe the probe is placed in. The best-case scenario puts most of the best industrial transmitters somewhere between -40°C and +85°C. A few specialized varieties may go as high as +125°C or higher.
- Shock and vibration resistance. Bulky machinery would rather ignore sensitive electronics. Observation of compliance with IEC 60068-2-6 (sine vibration, normally 20 5 Hz to 2, 25 Hz g from 2 kHz) and IEC 60068-2-64 (random vibration, usually 7.5 g_rms from 5 Hz to 1 kHz) for particularly angles. The shock resistance has to be at least 20 g/11 ms in accordance with IEC 60068-2-27.
- Corrosion resistance. The enclosure and thermowell must resist the environment and the atmosphere. AISI 316L stainless steel is intended for general industrial use. Hastelloy C is an are to strong acids and chlorides, and Inconel to high-temperature oxidation. Grade 2 is used for handling seawater and its aggressive chemicals.
- Area classification certification. Transmittors intended to measure in the oil, gas, and chemical industry must be given ATEX or IECEx certification. Explosion-proof (Protected Ex d) houses cannot perform an internal ignition within the required USee table. Intrinsically safe (Protected Ex ia) designs restrict the electrical energy level to magnitudes still lower than any ignition threshold. For some safety-critical loops, SIL 2 or SIL 3 certification under IEC 61508 may be required.
EMC and RFI immunity are terms often bandied about. The industrial sector is fraught with electrical disturbances. Motors, drives, and radio equipment are notorious for interfering with and destroying the fragile sensor signals. In designing harsh-environment transmitters, all means must be in place like shielding, filtering, and grounding that can keep the signal intact.
Want to see how Black Ant’s temperature transmitters are built for these conditions? Our range covers Pt100, Pt1000, and thermocouple inputs with 4–20mA and HART output options, rated for process temperatures from –200°C to +1,200°C depending on sensor type. Explore our temperature transmitter specifications →
Black Ant also manufactures a complete line of industrial pressure transmitters, differential pressure transmitters, liquid level transmitters, and flow meters — so you can specify temperature, pressure, level, and flow from one certified supplier.
Sensor Selection in Harsh Environments: RTD vs Thermocouple
The transmitter is only half the story. The sensor at the process boundary has to survive the same punishment. And the choice between an RTD and a thermocouple will make or break your measurement.
RTD (Pt100 / Pt1000): Accuracy and Stability
Resistance temperature detectors, usually Pt100 or Pt1000, deliver the best accuracy and long-term stability in industrial temperature measurement. A Class A Pt100 gives you ±0.15°C accuracy at 0°C per IEC 60751. Over time, drift is typically less than ±0.1°C per year.
The disadvantage RTDs have over us is their higher susceptibility to mechanical damage. The sensing element, made of platinum, is actually a thin wire or film that is easy prey to its two main enemies: vibration and thermal shock. In cases where there is intense vibration—machinery like turbines, compressors, diesels—you must install a special, vibration toughened RTD assembly, or else your appliance will die with a premature death.
The temperature is yet another barrier. Standard Pt100 RTDs are good between –200°C to +850°C. There are some specially designed constructions that can go up over +1,000°C, but really it’s pushing the technology for RTDs.
Go for an RTD when temperature can be controlled within 600°C, the process requires high radiation, and the vibration level is fairly low.
Thermocouple: Ruggedness and Extreme Temperature
Thermocouples are self-powered junctions of dissimilar metals. They have no delicate wire coil to break. That makes them far more tolerant of vibration, shock, and rapid thermal cycling.
Their temperature range is unmatched. A Type K thermocouple works from –270°C to +1,260°C. Type B pushes past +1,800°C. These ranges are defined by IEC 60584. If you’re monitoring furnace flue gas, molten metal, or gas turbine exhaust, a thermocouple is usually your only practical choice.
Trade-offs represent accuracy and drift. Base-metal thermocouples undergo drift of 1–2°C per year in oxidizing environments. These copper–constantan and iron–constantan thermocouples provide output signal of a few millivolts that is highly sensitive to electrical noise and wiring errors unless used with quality transmitters at the sensor head.
Consider using a thermocouple when your application is above 600°C, there is high vibration, or a fast response time is needed.
RTD vs Thermocouple Harsh Environment: The Sensor + Transmitter Answer
In modern industrial practice, it is fallacious trying to run a raw RTD or TC signal from a couple of feet to hundreds of meters to the control room, the fiery furnace where volatile organic compounds could be inadvertently released into the air. In an industrial environment, the most likely solution is a sensor plus transmitter product for severity situations.
With the transmitter atop the sensor’s head, the weak signal is converted into a robust 4-20 mA or digital output. This resolves the problem of noise sensitivity that thermocouples suffer from, compensates for RTD lead-wire resistance, standardizes wiring, and gives you HART, all through a single connection cable.
Decision framework:
|
Condition |
Recommended Sensor |
|---|---|
|
Process < +600°C, precision critical |
RTD (Pt100 / Pt1000) |
|
Process > +600°C or high vibration |
Thermocouple |
|
Both scenarios |
Pair with a head-mount or field-mount transmitter |
When at a catalytic cracking petroleum plant in Southeast Asia the maintenance team switched from directly connecting thermocouple extension wire to mounting state-of-the-art field HART transmitters directly onto their reactor vessels, the loop noise, now cut 80%, went silent. The plant also gained more visibility over the health of the process, effectively cutting unplanned trips to the field by a good 50%.
Mounting Styles: Head-Mount vs Field-Mount vs DIN-Rail

Where you put the transmitter matters as much as what’s inside it. Harsh environments favor certain mounting styles over others.
Head-Mount Transmitters
This hockey-puck-styled temperature transmitter is sleek and fits right into the head of the sensor directly. The Pt100 thermal transmitter sits only an inch from the process; hence, it is protected against the harsh condition from any type of thermowell assembly, making it suitable for mechanical rooms and building automation.
- Pros: The device is super compact. The long lead wires from the sensor make the resistance even better to electrical noise. In some cases, this head-mount system may be cheaper than buying back-mains from the transmitter. Certainly, no cost would come for an additional housing and housing mounting brackets.
- Downside: The ambient conditions at the point of measurement will be shared by the transmitter. If the process area is running so hot, conductive heat can increase the temperature at the head to levels exceeding the transmitter’s ambient temperature rating. It is not unusual for the head to reach +85°C and beyond. In these cases, the process would require an elongation nipple, cooling fins, or the removal of altogether different mounting.
- Recommended Application: Space-constrained mechanical rooms, gardening boilers noted for moderate heat, chemical reactors where the sensor head would not exceed its ambient limits, and applications where price and simplicity are more meaningful.
Field-Mount Transmitters
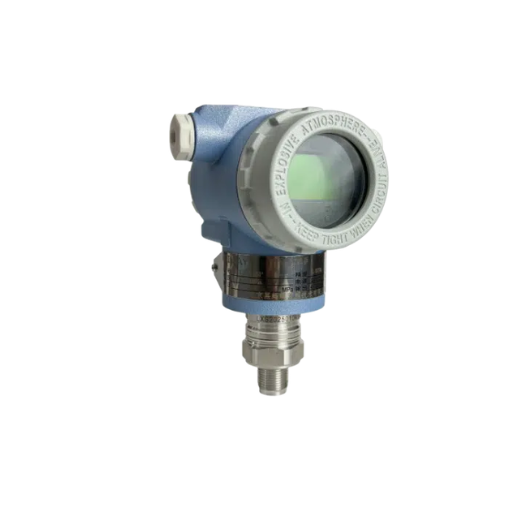
Field-mounted transmitters come in one and the same rugged sealed housing with two compartments from time to time, normally die-cast aluminum or 316L stainless steel. They are mounted on a pipe or a wall close to the sensor with a short length of sensor cable connected to them.
- Pros: They have been designed to survive severe treatment. They are standardly certified IP67 or IP68. Explosion-proof certifications come less frequently. A dual-compartment design is important as it will allow you to open the wiring cover without exposing the circuit board in the rain. Most units also come with a local LCD display for the field reading.
- Cons: Relatively large and expensive with a requirement for mounting hardware and a short sensor cable length.
- Best used: Offshore platforms, outdoor pipelines, high vibration compressors, washdown areas in food plants, etc., where access to measurement points is difficult or are nearest to heat packages.
DIN-Rail Transmitters
DIN-mounted transmitters are mounted within electrical cabinets or control rooms. These are direct-connected to sensor cables and convert signals.
- Advantages: Protection from field conditions assures long life. They afford easy access for calibration and troubleshooting activities. This is usually the cheapest option per channel.
- Limitations: Long sensor cable runs are vulnerable to electric noise and ground loops in harsh plants. The transmitter’s far placement from the process means that the noise immunity advantage of local conversion is lost.
- Ideal for: Clean electrical rooms, laboratory control panels, and applications where the sensor is already wired back to a controlled cabinet.
Head Mount vs Field Mount Temperature Transmitter: Selection Summary
|
Factor |
Head-Mount |
Field-Mount |
DIN-Rail |
|---|---|---|---|
|
Environmental protection |
Good (protected by sensor head) |
Excellent (IP67/IP68, dual-compartment) |
Poor (IP20, cabinet-dependent) |
|
Vibration resistance |
Moderate to good |
Excellent |
N/A (not in field) |
|
Accessibility for maintenance |
Moderate |
Excellent |
Excellent |
|
Local display |
Rare |
Common |
Rare |
|
Cost |
Lowest |
Highest |
Low |
|
Best applications |
Mechanical rooms, moderate harshness |
Offshore, extreme heat, high vibration, outdoors |
Protected control rooms |
Industrial Temperature Transmitter Selection: Critical Criteria for Harsh Environments

Once you’ve chosen your sensor type and mounting style, the real engineering work begins. Here’s what to verify before you issue a purchase order.
Ingress Protection and Enclosure Materials
IP encapsulations variations can be achieved by cloth with a given so-called kick sequence.
- IP65: protection against harmful dust amounts that left a low-pressure water spray from any direct rain. Suitable for most industrial indoor installations.
- IP67: protection against harmful dust amounts with temporary immersion over 1 m depth under water. The standard for single-use wash areas like fountains.
- IP68: a degree which defines a housing as perfectly water-tight, or water enters his feet and lodges to a half-inch depth then falls without doing any harm. It is important for pump tanks, wet wells, and some marine installations.
The IP code and then material of the enclosure to come from matter. This is especially an issue in harsh environments, especially corrosive atmospheres. A thick anti-corrosive coating of aluminum die-cast corrosion with so many industrial settings is recommended, whereas the industry would not have anything much better than 316L stainless steel for offshore platforms, chemical plants, and coastal installations.
Temperature Ratings and Thermal Management
There are two basic temperatures to be considered; that is, the process temperature (the flow fluid you are measuring) and the ambient temperature (the air around the transmitter electronics).
A transmitter rated for –40°C to +85°C ambient moves into sterile ambient if you expect to bolt it on directly to a 600°C pipe. The clear solution to this is thermal isolation:
- Extension nipples: Increase the length between the hot process connection and the transmitter housing.
- Cooling fins: Disperse heat from the transmitter housing.
- Remote mounting: Use a field-mount transmitter away from the heat source.
Historically use the manufacturer’s derating curves! Though the transmitter may be rated to +85°C ambient based off an extension length, when an extension length is minimized, the temperature extremes may be down to +60°C only.
Vibration and Mechanical Shock Resistance
Almost every industrial standard implies vibration tests. The following is a practical explanation of the numbers:
- IEC 60068-2-6 (sinusoidal vibration): 20 g from 25 Hz to 2 kHz—the continuous vibration of some giant compressor or turbine.
- IEC 60068-2-64 (random vibration): 7.5 g_rms from 5 Hz to 1 kHz-frequency response simulates the broadband vibration of vehicles, ships, and rotating machinery.
- IEC 60068-2-27 (shocks): 20 g/11 ms is harsh but realistic for impacts during transport, installation, or sudden closing of a valve, etc.
Provided your transmitter will spend the rest of its working life on a diesel generator, gas turbine, or cement kiln, these certifications become essentially compulsory.
Corrosion Resistance and Wetted Materials
The thermowell and any process-wetted parts must survive the chemistry of your fluid. Here’s a quick reference:
|
Material |
Best For |
Avoid |
|---|---|---|
|
316L stainless steel |
General industrial, water, mild chemicals, food and beverage |
Strong chlorides, hydrochloric acid |
|
Hastelloy C |
Strong acids, chlorides, oxidizing chemicals |
Caustic soda at high concentration |
|
Inconel 600 |
High-temperature oxidation, furnaces, flue gas |
Reducing acids |
|
Titanium |
Seawater, hypochlorite, nitric acid |
Hydrofluoric acid, concentrated sulfuric acid |
|
Ceramics (AL2O3) |
Extreme abrasion, some acids |
Thermal shock, impact |
For high-temperature applications, remember that 316L stainless steel is rated for continuous use in air up to about 650°C. Above that, you need Inconel or specialized high-temperature alloys.
Output Signals and Communication Protocols
The resultant choice ultimately depends on the control system applied and how much you loathe walking out to the field for sensor replacement or diagnostics.
- When you look at the larger plant view, 4–20 mA ensures good digital industrial performance. Starting with an analog loop, temperature transmitter 4-20mA HART output is free from susceptibility to voltage drop over long runs of cable and communicable with every PLC, DCS, or BMS analog input card.
- HART is present. This works hand-in-hand with physical 4-20 mA while concurrently transmitting digital data to it. This is for configuration and viewing at a remote location (albeit slowly). When the control system is on the spot and children have never known what a train is, HART should prove a good choice.
- Modbus RTU/RS485—Multidrop config. This is an end-to-end, digital-type network setup. Looking at building automation and SCADA needs for one bus, look to this system. Good.
- WirelessHART is the way to go. With WirelessHART, you just take away all the cabling. Ideal for rotating equipment, remote tank farms, temporary installations.
The temperature-transmitters from BlackAnt are known to have the standard support for the 4–20 mA and HART values, integration options for RS485 and Modbus being present, along with integration with some third-party BMS and SCADA systems.
Need a temperature transmitter that talks to your existing control system? Black Ant instruments support 4–20mA, HART, and Modbus RTU out of the box. Download the full technical documentation package →
Hazardous Area and Safety Certifications
Certification becomes binding if the plant deals with flammable gases, vapors, or dusts.
- Explosion-proof (Ex d): Housing is so constructed that it can withstand an internal explosion without igniting the surrounding atmosphere. This is common in Zone 1 and Zone 2.
- Intrinsically safe (Ex ia): The transmitter and its associated barrier limit electrical energy to a level that cannot cause ignition. This is safe for Zone 0, 1, and 2. It is often a preferred choice since the equipment is lighter and easier to maintain.
- SIL 2 / SIL 3: Functional safety certification according to IEC 61508. This is required for safety instrumented systems (SIS) where temperature measurement failure could lead to a dangerous process condition.
Application-Specific Recommendations

Oil and Gas and Petrochemical
Industrial operations such as those on offshore platforms and refineries require field-mount HART transmitters that are placed within 316L or Hastelloy thermowells. Furnace and flare-stack monitoring at a temperature of over 1,000°C necessitates Type K or Type N thermocouples to connect out from the transmitters, in order to keep certain electronics from inevitably being damaged by the daunting radiant heat. One would usually find a safety loop certified with the SIL.
Medical gadgets and chemical applications
In both batch reactors and distillation columns, ±0.5°C accuracy, probably the widest choice for a Pt100 RTD, is required. For corrosive services, the mission might call for Hastelloy or titanium plungers. In washdown areas, it is the typical setup with the IP67 field-mount housing. The HART diagnostic alerts let the staff fix the sensor drift before sending a batch to a state of out-of-spec.
Energy and Metal Processing
The thermocouples would be the type whose job is monitoring boiler tubes, steam pipelines, molten metal baths, with temperatures anything from 500°C and reaching 1,500°C. Vibration resistance with turbines or compressors is necessary. Transmitters that are stationed far away and have cooling extension ease the job of keeping electronics from being cooked by the furnace heat.
Food and Beverages / Water Treatments
Pasteurization, CIPs, and tank farms are available, with 316L stainless steel for all wetted parts, for exceptional hygiene and corrosion resistance.
Standard tri-clamp connection. Transmitters (with optional IP67 or IP65 ratings) capable of surviving a washdown mode. Pt100 RTD readings are used for HACCP compliance standards.
Building Automation and HVAC
This is Black Ant’s core market. Chilled water, hot water, and steam systems in mechanical rooms typically operate well below +200°C. Pt100 or Pt1000 head-mount transmitters with 4–20 mA output integrate directly into PLC and BMS or BEMS analog input cards. Accuracy requirements are moderate, but reliability over years of pump vibration and seasonal temperature swings is essential.
At a mixed-use commercial building in Beijing, the facility manager replaced faulty direct-reading sensors with Topwing’s head-mount Pt100 transmitters in the chilled water loop. There were improvements in stable temperature controls and minimal false alarms to the maintenance team due to electrical noise from variable-frequency drives.
Installation Best Practices for Harsh Environments
If there is a mistake in transmitter installation then it can be termed as the best of all choices.
Instillation of the well: The probe must stick out far enough into the pipe so that it is within a fully developed flow regime. One generic (although totally fine) rule is that the stem should reach ten times the thermowell’s outer diameter. Too low down and it will measure the temperature of the pipe wall rather than the fluid. Too long and the resonance risk grows.
Grounding and shielding: In electrically noisy plants, you must run only one end of your cable shield to ground; typically this end would be at the control system so as to avoid ground loops. Follow the EMI grounding standard for your plant.
Cable glands and conduit sealing: Peer failures and equipment maintenance start with the right cable gland rating for IP/NEMA requirement. At explosive area locations, use Ex-certified cable glands. Keep the seal of the enclosure design to prevent ingress of moisture. Make sure your cable routes are built with a drip loop so water can’t track down into the enclosure.
Thermal protection – For high-temperature procedures, it is advisable to employ extension nipples towards the transmitter electronics within the temperature parameter. It should never be screwed down directly against a surface that exceeds the range specified.
Calibrations, intervals, and their importance – The harsh environment can speed up the process of calibration drift, so you require to have thermocouple calibrations every 6–12 months and RTD calibrations every 12–24 months as per planning. HART diagnostics could, by then, enable you to catch drift in due time to lengthen calibrations where hazards permit.
For deeper guidance on industrial temperature measurement theory and practice, consult the Endress+Hauser Industrial Temperature Measurement Handbook.
Temperature Transmitter Specification Checklist

Use this checklist before you issue a purchase order:
- Process temperature range and selected sensor type (RTD or thermocouple)
- Ambient temperature rating for transmitter electronics
- IP/NEMA rating matched to environmental exposure
- Wetted materials compatible with process media
- Vibration and shock test certifications (IEC 60068-2-6, IEC 60068-2-64, IEC 60068-2-27)
- Output signal: 4–20mA, HART, Modbus RTU, or wireless
- Hazardous area certifications (ATEX/IECEx/SIL) if required
- Mounting style: head-mount, field-mount, or DIN-rail
- Process connection: threaded, flanged, or sanitary tri-clamp
- Accuracy and long-term stability specifications
- Supplier support: documentation, calibration service, spare parts availability
Conclusion
It is but a matter of practicing pragmatism that makes the choice of industrial temperature sensor easier for rated industrial environments from caustic effects: Users will want to align equipment capabilities with the conditions that exist in the field.
To begin with, the sensor. On the RTD vs thermocouple harsh environment question, the Pt100 temperature transmitter is the choice for high precision below +600C. Extreme heat or severe stress of vibration is more likely to call for the use of thermocouples. It gets protected through the electronics. As loudly vies of head mount vs field mount temperature transmitter, a head-mount configuration should be kept into mind for tight mechanical rooms while field-mount would be a better option for offshore platforms or washdown areas. Please verify your request for remote diagnostics without problems with extra cabling in a 4-20mA HART output with a temperature transmitter selected to perform this function. Choose the proper process chemistry of the wetted materials. Confirmed IP rating compliance, vibration certification, and hazardous-area approval are essential.
A properly selected temperature transmitter should only perform well on day one but also after three years: across thousands of thermal cycles, thousands of hours of vibrations, numerous hours of pressure cleaning.
Ready to specify a temperature transmitter that holds up in your harshest applications? Black Ant manufactures Pt100, Pt1000, and thermocouple-input temperature transmitters with 4–20mA and HART outputs, rated for process conditions from –200°C to +1,200°C. Our ISO 9001-certified production and CE-compliant documentation mean you can specify with confidence for projects across Europe, Asia, and the Middle East. Request a datasheet and application support →