How Differential Pressure Transmitter Filter Monitoring Optimizes HVAC and Industrial Performance
The HVAC system at manufacturing facility which spans 200000 square feet outside Shanghai exceeded its energy consumption limit by 30 percent. Facility manager Li Wei had checked every component. The chillers received maintenance. The pumps achieved their required operational balance. The control sequences followed the specification exactly. Yet the energy bills kept climbing.
The culprit turned out to be something deceptively simple: filters. The filters did not need repair because they were both present and operational. The filters appeared clean to the eye but their actual condition caused a 0.4-inch water column resistance increase to the system. The small system pressure difference created a need for supply fans to operate at higher capacity which resulted in increased electricity costs of ¥180000 per year. Li replaced the filters and installed differential pressure transmitters to monitor loading in real time. The energy consumption reached its standard level again after six months, and his team developed a reliable system for determining when to replace filters.
If you’re managing HVAC, compressed air, or process filtration systems, you have probably faced this same dilemma. Changing filters before their necessary time results in wastage of both materials and employee work time. Changing filters after their replacement date will result in expenses, equipment damage, and potential problems with indoor air quality. Better measurement provides the solution to the problem instead of improved scheduling operations.
The guide demonstrates how differential pressure transmitter filter monitoring system enables maintenance work to shift from time-based predictions toward accurate assessment of actual system status. The structured information will show you all details about the operational principles, best methods for installation, and benefits obtained from DP monitoring for building management and industrial control systems.
What Is a Differential Pressure Transmitter?

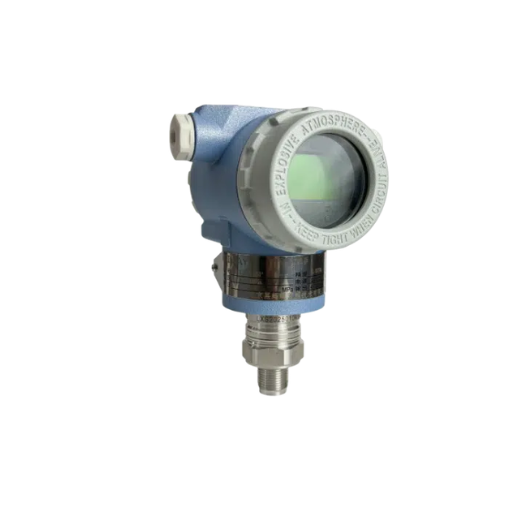
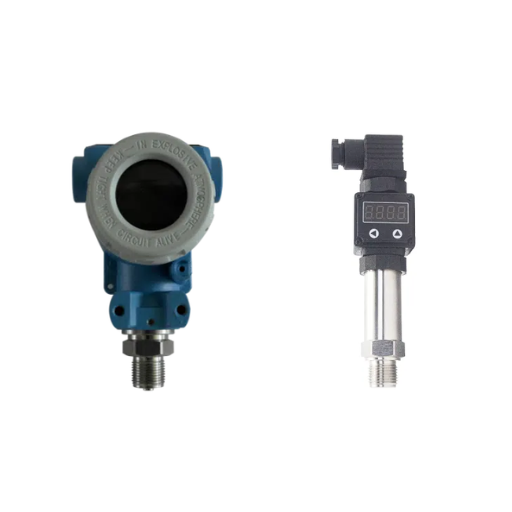
A differential pressure transmitter operates as a device which measures pressure differences between two points in a fluid system and produces an electrical signal according to established standards. Differential pressure transmitter filter monitoring utilizes this technology to provide real-time updates about filter loading status. A DP transmitter functions by measuring the pressure difference between two pressures which it receives through its two input points while a gauge pressure transmitter measures pressure according to atmospheric conditions and an absolute pressure transmitter measures pressure according to vacuum conditions.
The transmitter connects to the pressure taps which exist on both sides of the filter media in filter monitoring applications. The high-pressure port senses the upstream pressure before the filter. The low-pressure port senses the downstream pressure after the filter. The filter begins to capture particulates which results in increased flow resistance and this causes the pressure drop across the media to rise according to a directly proportional relationship. The transmitter detects this change and the system produces an output signal which typically operates within the range of 4 to 20 milliamps and 0 to 10 volts and supports HART or Modbus digital communication protocols.
Black Ant’s differential pressure transmitters provide measurement capabilities which range from 0 to 25 pascals for low-resistance HVAC filters and up to 100 kilopascals for industrial process applications. The accuracy standards permit measurements with a range of ±0.5% of full scale for critical cleanroom monitoring and ±1.0% for general HVAC service. All models carry CE certification and feature stainless steel wetted parts which can handle air and non-corrosive gases and liquids according to their specific design.
The transmitter contains a sensing element which uses a capacitive or piezoresistive diaphragm as its main component to detect pressure changes through physical diaphragm movement. The mechanical movement of the system uses high-precision electronics to produce an electrical output signal. Industrial transmitters use modern temperature compensation systems to maintain accuracy across all temperature ranges between –40°C and +125°C while standard HVAC systems use the technology across their operational range of –20°C to +70°C.
How Differential Pressure Transmitter Filter Monitoring Detects Clogging
A differential pressure transmitter detects filter clogging through its ongoing measurement of hydraulic resistance which filter media generates. Clean filter material presents minimal resistance to flow. The obstruction develops from particle accumulation which occurs in both media pores and surface areas, thus requiring increased upstream pressure to sustain identical flow.
The basic principle follows this relationship:
|
Filter Condition |
Upstream Pressure |
Downstream Pressure |
Differential Pressure |
|---|---|---|---|
|
Clean filter |
Low |
Similar to upstream |
Minimal (baseline) |
|
Partially loaded |
Increasing |
Decreasing relative to upstream |
Rising |
|
Fully clogged |
High |
Significantly lower |
Maximum (alarm threshold) |
|
Filter failure/bypass |
Equalized |
Equalized |
Near zero |
The transmitter detects pressure differences through its two ports because its internal sensing diaphragm only reacts to these differences. The measurement remains unaffected by line pressure because it operates between 10 pascals and 10,000 pascals. The transmitter measures only the pressure difference which engineers express as ΔP = P₁ – P₂ with P₁ as upstream pressure and P₂ as downstream pressure.
Marcus Chen established a pharmaceutical cleanroom at his Suzhou facility which he built with new cleanroom construction. The initial filter differential pressure readings showed 45 pascals across the HEPA bank because he used HIS monitoring system. He established clean filters at design airflow as his filter baseline. The monitoring system activated maintenance alerts after differential pressure reached 250 pascals which the manufacturer considered to be the maximum safe limit. The transmitter reading reached 248 pascals after 147 days of operation which resulted in a work order being triggered. The maintenance team performed the filter replacement on the following day after receiving the filters during a production pause. The system recorded no contamination incidents. The system operated without needing any emergency shutdowns. The DP transmitter provided four months of early detection which enabled the team to perform maintenance tasks before any problems occurred.
Establishing baselines enables straightforward signal interpretation for the following analysis. Normal loading conditions produce a continuous output which shows a gradual increase. An abnormal event occurs when there is a sudden spike because that indicates a collapsed filter media or an upstream release of particulates. A drop to zero or near-zero differential pressure indicates a filter breach, gasket failure, or bypass condition where unfiltered air is passing around the media. Continuous DP monitoring enables different maintenance responses which are triggered by three distinct operational conditions.
Key Benefits of Differential Pressure Transmitter Filter Monitoring

Energy Efficiency and Cost Reduction
The relationship between filter loading and energy consumption shows a direct connection which can be measured. The fan blower or compressor needs to increase its operational capacity for each pressure drop that occurs across a filter to sustain airflow. HVAC systems experience two to three times greater pressure drop when a filter reaches 80% of its service life compared to a clean filter. The fan law equations demonstrate that power consumption rises with pressure in constant-volume systems because even minor pressure increases result in excessive energy costs.
Research from the Building Technologies Office demonstrates that facilities implementing differential pressure-based filter monitoring achieve energy savings of 20 to 30 percent compared to facilities using fixed replacement schedules. These savings come from two sources. First, filters remain in service for their full useful life rather than being discarded prematurely based on calendar intervals. Second, filters are replaced before they reach the steep portion of the pressure-drop-versus-loading curve where energy penalties accelerate.
The economic benefits of the system apply specifically to compressed air systems. The study results show that every 2 pounds per square inch increase in filter differential pressure results in a 1 percent rise of energy costs. The 37-kilowatt compressor operates 6,000 hours per year which results in electricity costs of approximately €33,300 at a rate of €0.15 per kilowatt-hour. The annual energy penalty for that single compressor exceeds €1,600 because poor filter management creates 10 psi of unnecessary pressure drop.
Black Ant’s DP transmitters use standard 4-20mA and Modbus outputs to connect directly with building management systems. This connection allows automatic monitoring of filter loading across air handling units and compressed air stations and process filtration skids. The energy management dashboards use data feeds to show real-time energy costs which result from filter condition. This system enables businesses to monitor filter condition, which helps them assess their return on investment in monitoring hardware.
Maintenance Optimization and Equipment Protection
Scheduled replacement programs for filter maintenance therefore show higher maintenance costs which range from 35 to 40 percent compared to predictive maintenance that uses differential pressure monitoring. The cost savings result from two factors which include the elimination of unnecessary work and filter materials that remain unused because actual usage has not reached maximum limits and the removal of emergency service needs which arise from blocked filters that trigger system alarms and damage equipment.
The process of extending filter life produces measurable results which benefit various operations. When replacement timing is optimized based on actual loading rather than conservative schedules, filter service life typically extends by 20 percent or more. This is not achieved by running filters beyond their capacity. The system enables users to retain filters until their actual capacity reaches its full potential instead of disposing them based on predetermined dates.
Equipment protection represents the third major benefit category. Clogged filters in HVAC systems can cause reduced airflow, coil freezing, and compressor damage. In compressed air systems, excessive pressure drop can overload compressor motors and reduce air dryer effectiveness. In hydraulic systems, high filter differential pressure can trigger bypass valves, which allow unfiltered fluid to reach sensitive components. DP transmitters provide early warning before these failure modes develop, enabling intervention that protects capital equipment.
Compliance and Documentation
For facilities subject to regulatory oversight, differential pressure monitoring provides documented evidence of maintenance performance. Cleanroom operations under ISO 14644, pharmaceutical manufacturing under GMP guidelines, and healthcare facilities under infection control standards all require verifiable air filtration performance. A continuous DP monitoring record demonstrates that filters were maintained within specified pressure drop limits, supporting audit requirements and regulatory submissions.
Want to see how DP monitoring integrates with your existing BMS? The differential pressure transmitter specifications of Black Ant show how their standard 4-20mA and Modbus outputs work with your control platform.
Installation Best Practices
Pressure Tap Placement
The correct installation process begins with identifying the correct location of the pressure tap. The high-pressure port connects to the filter’s upstream section, which exists before the filter’s media. The low-pressure port connects to the downstream side, after the media. This configuration enables the transmitter reading to increase whenever the filter loads because greater differential pressure indicates more clogging.
The appropriate location for pressure taps exists on the sides of ductwork or pipework systems instead of their bottom sections. Side mounting prevents the accumulation of sediment or condensate in the impulse lines, which can cause measurement errors or line blockage. Taps should be positioned at least five duct diameters upstream and two diameters downstream of any elbows, dampers, or transitions to ensure stable pressure readings representative of the filter condition.
Taps should be located at the center of rectangular ductwork’s duct face. The use of multiple taps in round ductwork enables accurate measurement through a piezometer ring, which provides average values for the duct cross-section while the system experiences different velocity profiles. The impulse lines that connect the taps to the transmitter need to be short because their length needs to match for accurate temperature measurement.
Impulse Line Design
The design of impulse lines for different fluids requires different approaches. The design requires lines to slope downward from the transmitter toward the process taps which should maintain a minimum grade of 1:12 for air and gas applications. The slope of the line system enables any condensate formation which occurs in the lines to flow back into the process instead of accumulating at the transmitter. The design for liquid applications requires upward sloping lines which direct gas bubbles back into the flow stream.
The selection of tubing diameter enables operators to choose between two competing requirements which need specific time and blockage resistance characteristics. The standard for clean air applications requires the use of quarter-inch tubing. The half-inch tubing option serves better for applications which experience heavy particulate contamination or which have faced problems with impulse line blockage. The larger diameter provides greater resistance to plugging while maintaining acceptable dynamic response for filter monitoring applications where changes occur over hours or days rather than seconds.
Condensate and seal pots serve as required installations for process taps in steam and high-temperature operations. The pots establish a liquid head system which protects the sensing element from high temperatures while supplying the transmitter with a pressure reference point. The pots require water or condensate filling before startup which creates a liquid seal that protects the transmitter from process temperature.
Mounting Considerations
The filter housing allows differential pressure transmitters to connect either through a manifold valve assembly or through remote installation which uses impulse lines to link with the process. The system should use direct mounting because it provides accessibility to perform transmitter maintenance and calibration in clean environments which produce low vibrations. The system should use remote mounting because high vibration environments and high temperature environments and locations with inaccessible transmitter units which require access behind the filter housing need transmitter units to be installed.
The installation of liquid service lines should be done below the process taps because this configuration keeps the lines full of liquid which delivers both stable measurements and quick responsiveness. The installation of gas or dusty application systems requires above process tap mounting which allows particulates to enter the impulse lines but fall back into the process instead of staying at the transmitter. The specific application conditions and maintenance access requirements will determine which mounting position should be used.
Black Ant’s differential pressure transmitters include manifold valve options that enable transmitter isolation, zero verification, and calibration without process shutdown. The three-valve or five-valve manifolds provide positive isolation of both high and low pressure sides plus an equalizing valve that brings both ports to the same pressure for zero calibration.
Commissioning and Calibration
Technicians need to determine both the zero point and the complete range of measurement when they commission a DP transmitter which monitors filter performance. The zero calibration process requires equal pressure to be applied at both transmitter ports which technicians achieve by opening the manifold equalizing valve while keeping the process isolation valves shut. The procedure should be conducted with the transmitter placed in its permanent installation spot because any change in elevation will impact the zero point through liquid head variations in the impulse lines.
Verifying span requires a known pressure differential which technicians create using a handheld calibrator or by connecting a reference gauge to the transmitter through a temporary parallel installation. Technicians need to validate the output signal at zero and at maximum differential pressure against the established transmitter specifications. The goal of filter monitoring systems requires operators to achieve precise results to monitor filter conditions because the process needs to measure filter conditions instead of actual flow rates.
The system needs to operate with clean filters after calibration because this step establishes the baseline differential pressure. This starting point serves as the base measurement which technicians will use to track filter accumulation throughout the monitoring period. The maintenance management system needs to document the baseline together with the alarm setpoints which initiate filter replacement work orders.
Applications Across Industries

HVAC and Building Automation
The buildings which include commercial and institutional spaces use differential pressure transmitters to measure filter loading in their air handling units and rooftop units and ventilation systems. The most common application is monitoring pre-filters and final filters in central station air handlers serving office buildings hospitals schools and retail spaces. Maintenance technicians can check filter status during their routine inspections through DP transmitters which have visual indicators and local displays without needing access to the control system.
Building management systems enable automatic filter management through their workflow integration functions. The BMS system creates a maintenance work order and notifies the facilities team through email and SMS when transmitter readings exceed the established setpoint, while it may also adjust fan speed to sustain airflow until maintenance work can begin. Facilities managers use historical data logging to study filter loading trends which helps them determine optimal replacement times based on changing outdoor air quality throughout different seasons.
DP transmitters which control variable air volume systems enable fan speed optimization. The VAV controller uses its ability to increase fan speed when filters become blocked, which creates higher system resistance. The system uses automatic compensation to keep people comfortable inside the building while it hides the extra energy costs caused by blocked filters. The DP transmitter shows the current filter status along with detailed information to maintenance staff, who will discover that replacing the filter will decrease energy usage because of high fan energy costs.
Cleanrooms and Controlled Environments
The verification process for HEPA and ULPA filter performance needs constant checking because pharmaceutical manufacturing facilities and biotechnology laboratories and semiconductor fabrication plants require it. The regulatory standards which include ISO 14644 for cleanrooms and EU GMP Annex 1 for sterile manufacturing demand documented proof that final filters maintain their required performance standards. The system uses differential pressure monitoring which operates continuously to document filter bank performance instead of depending on testing that occurs at scheduled times.
Cleanroom applications require higher precision measurements than standard HVAC operations. Black Ant’s differential pressure transmitters offer precision through their specifications which achieve ±0.5% accuracy and operate between 0 and 25 pascals to identify filter loading that impacts room cleanliness standards. The transmitters connect to environmental monitoring systems that log readings at regular intervals which generate trend reports for quality assurance reviews and regulatory audits.
Black Ant’s HVAC control product line uses pressure-independent control valves which work together with DP monitoring to sustain room pressurization. The control system in positive-pressure cleanrooms regulates supply and exhaust valves to create pressure differentials between the cleanroom space and adjacent areas. The control system needs constant monitoring because filter loading changes available pressure which affects contamination control.
Industrial Process Filtration
Manufacturing facilities use DP transmitters to monitor inline filters which protect pneumatic tools and instruments and production equipment. Compressed air filters work to eliminate particulates and moisture and oil aerosols that would harm downstream equipment. The total cost of a clogged air filter includes two components which are the increased energy expenses at the compressor and the risk of production downtime when air pressure falls below necessary levels for equipment operation.
Hydraulic systems depend on high-pressure filtration to safeguard their pumps and valves and actuators from damage which results from particulate contamination. Differential pressure indicators across hydraulic filters provide early warning of element loading before the filter bypass valve opens. The cost of a DP transmitter in high-value hydraulic applications which include machine tools and mobile equipment and industrial presses remains insignificant when compared to the equipment value which it protects.
Dust collection and air pollution control systems use DP transmitters to monitor baghouse and cartridge filter performance. The pressure drop across a baghouse filter increases as the dust cake builds on the filter media. Periodic cleaning pulses remove the dust cake and reset the differential pressure. Monitoring trends in baseline pressure after cleaning indicates when filter bags require replacement due to blinding or physical damage.
Data Centers and Critical Infrastructure
Data center cooling systems depend on consistent airflow through computer room air handlers and in-row cooling units. Filter loading reduces airflow which creates hotspots that threaten IT equipment reliability. DP transmitters monitor filter condition without requiring visual inspection in restricted access areas. The system enables data center infrastructure management software to track filter condition and cooling unit performance through its filter condition tracking system.
Smart city applications use environmental monitoring stations that deploy differential pressure measurement to protect their air quality sensors. Black Ant’s smart environmental monitoring stations which measure particulate matter gases and meteorological parameters use filtered sampling systems that need maintenance when loading rises. DP monitoring extends maintenance intervals and ensures data quality by alerting operators when filter performance degrades.
Technical Specifications and Selection Guide
Selecting the appropriate differential pressure transmitter for filter monitoring requires matching the instrument specifications to the application requirements. The following parameters guide proper selection:
Pressure Range
The transmitter range must accommodate both the clean filter baseline and the maximum allowable differential pressure at filter replacement. The measurement system loses its ability to measure when the filter becomes saturated because the system uses an undersized measurement range. The system measurement range must be oversized to eliminate the low-end measurement problem which affects clean filter baseline data.
|
Application Type |
Typical Clean Filter ΔP |
Typical Maximum ΔP |
Recommended Transmitter Range |
|---|---|---|---|
|
HVAC pre-filter |
25–50 Pa |
150–250 Pa |
0–250 Pa |
|
HVAC final filter |
50–100 Pa |
250–500 Pa |
0–500 Pa |
|
HEPA filter |
100–200 Pa |
400–600 Pa |
0–600 Pa |
|
Compressed air |
0.1–0.3 bar |
0.5–1.0 bar |
0–1 bar |
|
Hydraulic return |
0.5–1.0 bar |
2.0–3.0 bar |
0–4 bar |
In situations where the clean filter baseline remains undefined, you need to choose a transmitter that includes adjustable span functions or provides dual-range capabilities which deliver necessary measurement accuracy from their lowest point to their complete operational range.
Accuracy and Stability
Standard HVAC filter monitoring applications typically accept ±1.0% accuracy. Critical applications including cleanrooms, pharmaceutical manufacturing, and high-value process protection benefit from ±0.5% accuracy instruments. Long-term stability, expressed as drift per year, is equally important for applications where calibration access is limited. Black Ant’s DP transmitters specify stability of ±0.1% per year which ensures consistent performance between calibration cycles.
Environmental Ratings
The transmitter enclosure must match the installation environment. Standard HVAC mechanical rooms require IP54 protection against dust and water splashes. Outdoor installations, washdown areas, and harsh industrial environments require IP65 or IP67 ratings. Temperature ratings must accommodate both ambient conditions and any radiant heat from adjacent equipment. Black Ant offers models rated for –40°C to +125°C operating temperature for industrial applications.
Output Signals and Communication
Building management systems and industrial control platforms support various input types. The 4-20mA current loop remains the most common standard for analog signals, offering noise immunity and compatibility with virtually all controllers. The control system uses voltage outputs which operate at 0-10V and 0-5V but101main susceptible to electrical interference when cables extended over long distances.
Digital protocols provide additional capabilities beyond the process variable. The HART protocol enables two-way communication through the same wires which carry the 4-20mA signal for remote configuration and diagnostic queries. The Modbus RTU and BACnet MS/TP protocols provide digital building networks with direct system integration which does not require analog conversion. Black Ant DP transmitters are available with all standard output options to match existing control infrastructure.
Do you need assistance in choosing a suitable DP transmitter for your specific application? You can download the Black Ant Differential Pressure Transmitter Selection Guide or request a consultation with our application engineering team.
Integration with IoT and Building Energy Management Systems

Modern differential pressure transmitter filter monitoring extends beyond local indication to integration with comprehensive building energy management systems and industrial IoT platforms. Black Ant’s product portfolio enables seamless integration from the field sensor through edge processing to cloud analytics.
The differential pressure transmitter functions as the sensing layer which detects physical filter conditions and translates them into an electrical signal that enables ongoing observation. The 4-20mA output provides direct connection for standalone applications through BMS analog input card and local panel meter. Networked applications use Modbus output to establish digital links with superior system components.
The IoT Data Collection Terminal collects information from multiple DP transmitters and various field devices which include temperature sensors and flow meters and energy meters. The terminal supports RS485, M-Bus, and 4-20mA inputs, which transform various signals into common data packets that can be sent. Wireless uplink via NB-IoT or LoRaWAN eliminates the need for control wiring in retrofit applications or remote installations.
The Edge Data Acquisition Computer system operates with local intelligence since it handles sensor data through processing at the device itself. The edge computer uses its AI capabilities to create alerts and execute control functions while it processes data to identify and remove irregularities before sending information through the network. The 38,000mAh lithium battery enables the edge computer to function autonomously for six years with two-hour collection intervals which makes it suitable for deployment in areas without stable electricity and network access.
The system support multiple deployment methods because of its three distinct architectural components. A single DP transmitter enables basic monitoring through its connection to an existing BMS system. The IoT Data Collection Terminal can receive data from multiple transmitters to conduct multi-point data collection. Edge Data Acquisition Computers enable critical applications to perform immediate processing of data at local sites. The three methods send data to central dashboards which display filter conditions at various sites and produce maintenance forecasts and determine energy expenses linked to filter usage.
Cost-Benefit Analysis and Return on Investment
The process of implementing differential pressure monitoring for filter management needs an initial financial commitment for equipment and its subsequent setup and system connection work. The return on this investment comes from energy savings, maintenance cost reduction, and equipment protection.
Typical Investment Components:
|
Item |
Quantity |
Unit Cost |
Total |
|---|---|---|---|
|
DP transmitter with manifold |
1 |
$200–400 |
$200–400 |
|
Impulse line tubing and fittings |
1 set |
$50–100 |
$50–100 |
|
Installation labor |
4 hours |
$75/hour |
$300 |
|
BMS integration |
4 hours |
$100/hour |
$400 |
|
Total per filter location |
$950–1,200 |
Annual Savings Components:
The 500-kilowatt HVAC system consumes electricity at a rate of 0.12 per kilowatt-hour for its 4,000 hours of annual operation. The annual fan energy consumption of the system operates at approximately 0.12 per kilowatt-hour. The annual fan energy consumption of the system operates at 240,000. The energy savings from optimized filter management reach $36,000 because filter replacements are performed at their proper schedule, which leads to a 15% reduction in energy usage.
Maintenance cost savings add to the benefit. The facility’s annual maintenance costs decrease by $15,000 when it operates 50 air handling units and removes two unnecessary filter changes that would occur each year at a cost of $150 for each change.
The combined annual benefit of 51,000 against an investment of approximately 51,000 against an investment of approximately 50,000 for outfitting 50 filter locations yields a simple payback period of 12 months. After payback, the continuous savings create pure return on investment.
The economic advantages maintain their strong appeal for smaller facilities and single-system applications. The 75-kilowatt compressed air system of a small manufacturing facility enables payback through energy savings within 18 to 24 months, which does not include maintenance optimization or equipment protection benefits.
Conclusion

The calendar-based management system creates an unsatisfactory solution that fails to meet the needs of any user. The early replacement of filters results in the loss of operational capacity which includes both the filter materials and the associated labor expenses. The costs of energy consumption and equipment damage together with the risk of system breakdowns increase when you wait to replace equipment until it no longer functions. Differential pressure transmitter filter monitoring provides continuous accurate measurement of actual filter condition which removes the need for a compromise solution.
The technology is not new. Industrial processes have used DP transmitters for process monitoring during the last three decades. Building automation systems now provide better access to the technology while the interface system enables users to monitor filter data which supports their complete energy management systems. Differential pressure transmitter filter monitoring provides various output options which include basic 4-20mA output and digital Modbus and wireless IoT connectivity for both small commercial systems and large industrial systems.
The benefits are quantified and proven. Facilities that use differential pressure measurement to monitor filter conditions for their systems will see their energy consumption linked to filter use decrease by 20 to 30 percent and maintenance expenses drop by 35 to 40 percent while their equipment durability increases. The improvements generated through these solutions reach a major level. The total operational enhancements from these solutions will return monitoring costs after one complete year of use.
Black Ant’s differential pressure transmitters provide all necessary components which include accurate measurement systems and dependable systems together with system integration functions needed to operate modern differential pressure transmitter filter monitoring systems. The CE-certified instruments which ISO 9001 quality management approved for manufacturing purposes enable users to connect building management systems through standard interfaces such as 4-20mA and HART and Modbus and BACnet. Black Ant provides its OEM partners and global distributors with private-label production services that include custom protocol development and complete engineering assistance.
Ready to optimize your filter management? Request a quote for differential pressure transmitters configured for your specific application, or download the technical datasheet to review specifications and integration options.